
High-Carbon Ferromanganese: Grade Bands, Cost Drivers and Acceptance
Leave a message
Ferromanganese and Its Three Carbon Families
Ferromanganese is the standard manganese carrier for steelmaking and foundry work. It is produced by reducing manganese ore with carbon and, in the refined grades, by further treating the high-carbon product to strip carbon out. Manganese is present in virtually every commercial steel because it combines with sulphur, controls the sulphide shape, and contributes solid-solution strengthening and hardenability. The tonnage of ferromanganese therefore tracks crude steel output more closely than almost any other ferroalloy.
The metal is not one product but three commercial families, distinguished by carbon content. High-carbon ferromanganese carries carbon in the 6-8% band and is smelted in blast furnaces or large electric furnaces from ore plus coke. Medium-carbon ferromanganese brings carbon down to the 1-2% band, and low-carbon ferromanganese goes below roughly 0.7%. The lower the carbon, the more refining steps are needed and the higher the price per tonne of contained manganese, because carbon removal costs energy, oxygen and time, and it usually also costs manganese yield.
It follows that a ferromanganese negotiation is really a negotiation about three variables at once: manganese content, carbon band, and phosphorus level. Price per tonne of alloy only becomes comparable once all three are pinned down.
Designations and the Grade Table Buyers Should Fix in Writing
Chinese national standard GB/T 3795 specifies ferromanganese designations and chemical requirements. The designation combines the material name with nominal manganese and a carbon code, so FeMn78C8.0 denotes a high-carbon grade at about 78% Mn with a carbon ceiling of 8.0%, while FeMn78C2.0 belongs to the medium-carbon family and FeMn80C0.7 to the low-carbon family. The requirements that matter commercially are the manganese minimum, the carbon maximum, and the phosphorus maximum, with sulphur and silicon usually treated as pass-or-fail maxima.
The table below sets out the bands in which most tonnage trades, expressed as typical industry ranges for tender comparison. A contract specification should replace these ranges with the agreed guaranteed values and the analytical method to be used.
| Family | Typical designation | Mn (%) | C (%) | Si max (%) | P max (%) | S max (%) |
|---|---|---|---|---|---|---|
| High carbon | FeMn78C8.0 / FeMn74C7.5 | 74.0-82.0 | 6.0-8.0 | 2.0 | 0.20-0.35 | 0.03 |
| Medium carbon | FeMn78C2.0 | 75.0-80.0 | 1.0-2.0 | 2.0 | 0.20-0.35 | 0.03 |
| Low carbon | FeMn80C0.7 | 78.0-85.0 | 0.30-0.70 | 1.5 | 0.15-0.30 | 0.03 |
| Low carbon, refined | FeMn85C0.4 | 83.0-88.0 | 0.20-0.40 | 1.5 | 0.15-0.25 | 0.03 |
Two observations follow directly from the table. First, moving from the high-carbon to the low-carbon band raises the manganese content at the same time as it lowers carbon, so a buyer cannot compare the two on alloy mass; the comparison must be made on contained manganese. Second, phosphorus is the element that most often decides whether a lot is acceptable, because phosphorus carried into the steel is not easily removed in the ladle and is particularly damaging in grades with low-temperature toughness requirements.
Very low phosphorus grades produced from selected low-phosphorus ore are traded as separate designations or as low-phosphorus variants of the same manganese and carbon combination, and they are priced at a clear premium. When a steel grade needs them, the requirement should be written as a phosphorus maximum, not as a general request for good quality material.
Manganese Ore: The Anchor of Ferromanganese Cost
Manganese ore sets the floor for any ferromanganese quotation. Four ore properties transmit directly into cost and into the specification of the alloy.
Contained manganese. Ore is traded and settled on contained manganese units, usually per dry metric tonne unit. A high-grade lump ore delivers more metal per tonne charged, which means less slag, less reductant and lower freight per contained unit than a low-grade ore.
Manganese-to-iron ratio. Iron in the ore dilutes manganese in the finished alloy. Ore with a low manganese-to-iron ratio forces the smelter to either accept a lower manganese content in the alloy or charge more ore to reach the guaranteed figure, and both routes cost money. This is why ore quality changes show up in ferromanganese price even when ore headline prices are flat.
Phosphorus. Phosphorus in ore reports almost entirely to the alloy. Ore with a low phosphorus-to-manganese ratio is the only practical route to low-phosphorus ferromanganese, so the premium attached to such ore becomes a permanent feature of the low-phosphorus alloy premium.
Physical form and moisture. Lump ore suits direct charging, while fines require sintering, briquetting or pelletising before they can be used efficiently. Moisture is settled on a dry basis and affects freight economics. Each preparation step adds cost and losses that appear in the alloy price.
Because ore is the dominant input, ferromanganese offers are sensitive to ore price, ore grade availability, ocean freight and currency. A buyer who tracks only the alloy number is watching the tail of the animal rather than the head.
Smelting Routes and Why Carbon Band Drives the Process
High-carbon ferromanganese is made by carbothermic reduction. Manganese oxides are reduced progressively as the charge descends, and the resulting alloy is saturated with carbon because the process is carbon-rich by design. The product is tapped, cast and crushed. Blast furnace and submerged-arc electric furnace routes are both in commercial use, and the choice affects cost structure rather than the basic chemistry.
Medium-carbon and low-carbon ferromanganese cannot be obtained by simply reducing the carbon charge, because a carbon-poor charge will not reduce the ore. The standard industrial approach is to take high-carbon ferromanganese and remove carbon from it, most commonly by oxygen refining, which blows oxygen into the molten alloy and burns carbon out, or by silicothermic or similar refining routes in which silicon in a manganese-silicon melt reduces manganese oxide and the carbon content falls. Both routes consume energy and both lose manganese to the slag to some degree, which is precisely why the refined families carry a premium.
For a buyer, the practical implication is straightforward: the carbon specification is a cost driver, not a formality. Requesting the lowest available carbon when the steel grade does not require it transfers a refining premium onto the purchase price for no metallurgical return.
Quotation Basis: What Has to Be Normalised Before Numbers Can Be Compared
Ferromanganese offers are frequently quoted on different bases, and the basis can explain more of a price gap than the material itself. Five items should be normalised before any comparison.
Unit basis. Offers may be expressed per tonne of alloy or per tonne of contained manganese. The second normalises across grades and is the only sensible way to compare FeMn74C7.5 with FeMn80C0.7, but it is valid only when the guaranteed manganese content and analytical basis are stated.
Delivery basis. Ex-works, FOB, CFR and DAP prices are not comparable. Ocean freight, inland haulage, port handling, insurance and the transfer of risk all differ, and in bulky ferroalloy cargoes freight is a large share of landed cost. The Incoterm, the named port and the named place belong in the offer.
Tax and export charges. Whether the figure includes value-added tax, and which export charges apply, must be stated. Comparison should be done on a landed, tax-excluded basis.
Size fraction and fines allowance. A screened 10-50 mm product and a broad 10-100 mm product with a fines allowance are different articles. The nominal fraction, the oversize and undersize allowance, and the treatment of undersize at weighing should be agreed in advance.
Validity, quantity and adjustment. Ferroalloy offers normally carry short validity because ore, energy and freight move. The validity period, the tonnage bracket, the shipment window and any price-adjustment mechanism for delayed shipment should all be recorded.
Only after those five items are aligned does the remaining price difference represent something real: producer cost position, ore sourcing, energy tariff and margin.
Matching the Grade to the Steel: Carbon, Phosphorus and Recovery
High-carbon ferromanganese is the default addition for carbon and low-alloy steels, where the carbon it introduces is either harmless or useful. Medium-carbon and low-carbon grades are selected when the steel specification caps carbon and the manganese must be added late, typically during ladle treatment, so that carbon pickup cannot be corrected by decarburisation.
Recovery depends on addition practice. Coarse ferromanganese added to the tapping stream dissolves progressively and gives stable, predictable recovery; fine material added to a quiet bath may float or be entrained in slag. Because ferromanganese carries manganese rather than silicon, deoxidation has to be arranged separately, usually by adding ferrosilicon or silicomanganese before or alongside the manganese addition, or by relying on aluminium deoxidation in aluminium-killed grades. Adding ferromanganese into an oxidised bath simply loses manganese to the slag, which is the most common and most expensive operating mistake in manganese alloying.
Phosphorus behaves differently from carbon. It cannot be removed conveniently in the ladle, so the phosphorus level of the steel is essentially the weighted average of the phosphorus contributed by the charge and by the alloys. In grades with tight phosphorus limits, the correct answer is to buy low-phosphorus ferromanganese, and the extra cost should be evaluated against the cost of rejecting or downgrading finished steel.
Physical Form, Size Fractions, Packaging and Storage
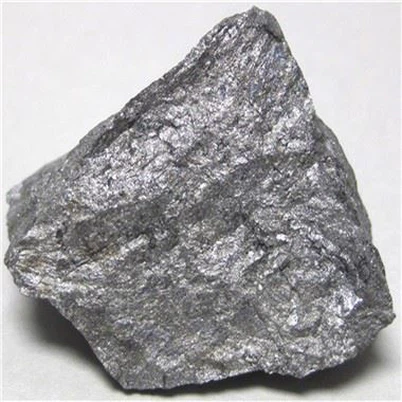
Ferromanganese is supplied mainly as crushed lump in fractions such as 10-50 mm, 20-80 mm and 10-100 mm, with finer 3-10 mm fractions used for wire feeding and powder injection. Particle size determination and reporting follow the applicable ferromanganese and ferroalloy particle-size test methods, and the particle size method used should be the one named in the contract so that the result is reproducible between seller, buyer and referee.
Fines are a genuine commercial issue, not a cosmetic one. Undersize material dissolves quickly but is easily lost to the slag and carries a higher surface area for oxidation during storage. Contracts therefore usually set an undersize allowance and a penalty mechanism, and the treatment of undersize at the weighing stage should be stated explicitly rather than left to practice.
Packaging options range from one-tonne woven bags and bulk liner bags, which suit container shipment and automatic charging, to steel drums and jumbo bags for smaller melt shops. Packing, marking, transport and the accompanying certificate are governed by the national standard for ferroalloy packaging, storage, marking and quality certificates, and the delivered certificate should identify the heat or lot, the grade, the chemical analysis, the size fraction and the net weight per package.
Storage practice is simple but consequential. Keep the alloy dry and separated by grade. High-carbon and low-carbon ferromanganese look similar in a bunker and behave very differently in the ladle, so mixing them silently destroys the carbon control that the purchase was designed to achieve. Alloy stored in wet conditions can also show surface oxidation and moisture pickup, which affects weight settlement; contracts usually settle on a dry basis or apply a moisture deduction.
Verification, Sampling and Acceptance
Sampling is the foundation of settlement. Sampling and preparation of ferroalloy samples is specified by ISO 3713, and the corresponding national sampling procedure for ferroalloy chemical analysis provides an equivalent route. Consignments are sampled as lots, the sample is reduced and divided, and the laboratory result defines payment. Without a defined sampling standard, two laboratories can legitimately report different values from the same lot, and the disagreement becomes a commercial dispute rather than an analytical one.
A workable acceptance structure for ferromanganese treats manganese as the settlement element, carbon as the grade-defining element with a maximum value, and phosphorus, sulphur and silicon as pass-or-fail maxima. Size distribution is inspected against the contracted fraction, and the moisture determination method and settlement basis are named. The contract should also state whether a referee laboratory may be appointed, and whether its result is binding.
Documentation should accompany every delivery: certificate of analysis traceable to the heat or lot, packing list with package weights, a size-fraction statement, and the transport documents. Weighing at destination against the seller's weights, with a stated tolerance, removes most post-voyage disputes before they start.
Comparing Offers and Managing Price Risk
The sequence below resolves most ferromanganese comparisons without guesswork.
Fix the required family and guaranteed chemistry first: manganese minimum, carbon maximum, phosphorus maximum, size fraction.
Normalise every offer to a single unit basis, expressed per tonne of contained manganese on guaranteed content.
Normalise delivery to a common Incoterm and named place, then add freight, insurance, port charges and duties to reach a landed, tax-excluded figure.
Convert size fraction, fines allowance and packaging commitments into a cost or loss figure so that a cheaper unscreened offer is not mistaken for a better one.
Check the sampling standard, certificate content and referee laboratory arrangements.
Check offer validity, shipment window and any price-adjustment clause, because the exposure between order and delivery is a real part of the price.
Review the supplier's historical analysis scatter, since consistent manganese and phosphorus results protect steel quality more than an attractive average.
Applied consistently, this approach normally shows that the landed cost ordering of ferromanganese offers differs from the ordering of their headline prices, and that most of the difference lies in grade normalisation, freight and phosphorus rather than in the alloy itself.
FAQ
Q: What is the difference between high-carbon and low-carbon ferromanganese?
They differ mainly in carbon content: the high-carbon family sits in the 6-8% carbon band and is made directly by carbothermic reduction, while the medium and low-carbon families are refined to reach roughly 1-2% and below 0.7% carbon. Refining costs energy and manganese yield, so the refined families carry a premium per tonne of contained manganese.
Q: Why is ferromanganese priced per tonne of manganese rather than per tonne of alloy?
Because manganese is the element being purchased and the grades differ widely in manganese content. Normalising to contained manganese makes FeMn74C7.5 and FeMn80C0.7 directly comparable, provided the guaranteed manganese content and the analytical method are stated in the offer.
Q: Which raw material influences ferromanganese cost the most?
Manganese ore, priced on contained manganese units and assessed on grade, manganese-to-iron ratio, phosphorus content and physical form. Ore grade and preparation route determine unit consumption, slag volume and reductant demand, so ore quality changes affect the alloy price even when ore headline prices are unchanged.
Q: What determines the phosphorus level in ferromanganese?
The phosphorus content of the ore, because phosphorus passes almost quantitatively into the alloy during smelting. Low-phosphorus grades therefore depend on selecting low-phosphorus ore, which is why they are traded at a premium and why a phosphorus maximum should be specified rather than implied.
Q: How should ferromanganese be added to the steel bath?
It should be added after deoxidation, typically into the tapping stream or during ladle treatment, so that manganese is not oxidised and lost to the slag. Addition into an oxidised bath wastes manganese, and fines added to a quiet bath are prone to loss, so the size fraction should be matched to the addition method.
Q: How is a ferromanganese consignment verified before payment?
By lot sampling and sample preparation following ISO 3713 or the equivalent national ferroalloy sampling procedure, followed by laboratory analysis against the contracted specification, with a certificate of analysis traceable to the heat or lot, a packing list, a size-fraction statement and destination weighing against a stated tolerance.