
Ferrovanadium Applications in Steel — Grade Selection by Steel Type
Ferrovanadium is added to steel to strengthen it and refine the grain through vanadium carbonitride (V(C,N)) precipitation. In microalloyed steels a small vanadium addition (commonly 0.02–0.15% V) raises yield strength, so mills meet strength grades with less carbon and better weldability. Vanadium dissolves into liquid steel during melting or ladle treatment, then precipitates as extremely fine V(C,N) particles during solidification and subsequent cooling. These particles impede dislocation motion through the ferrite matrix — precipitation strengthening — and pin austenite grain boundaries during thermomechanical processing, producing a finer ferrite grain size after transformation. The combined effect is a significant increase in yield and tensile strength without heavy alloy additions or high carbon content. Ferrovanadium is one vanadium product among several — it is distinct from vanadium pentoxide (V₂O₅) and vanadium nitride (FeVN), which serve different routes.
Ferrovanadium should not be confused with vanadium pentoxide (V₂O₅), an intermediate oxide used in chemical applications and certain extraction routes, nor with vanadium nitride (FeVN), which delivers both vanadium and nitrogen in a single addition and is sometimes preferred in specific rebar and bar mill applications where nitrogen control is favorable. The choice among these products depends on your melt shop practice, nitrogen levels in the base steel, and the specific mechanical targets you are trying to hit.
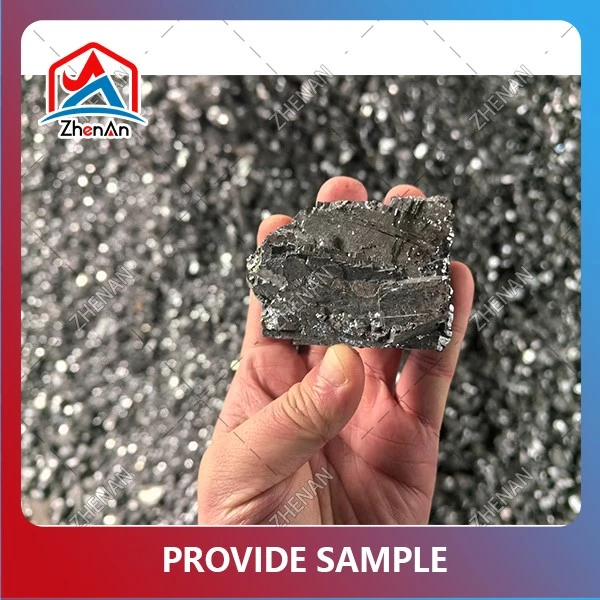
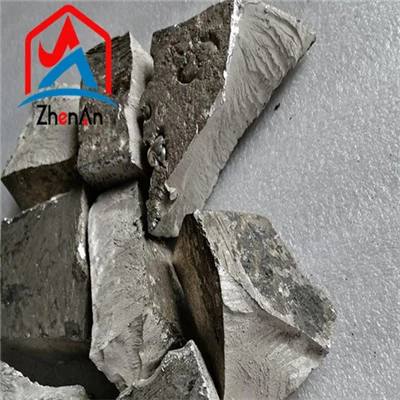


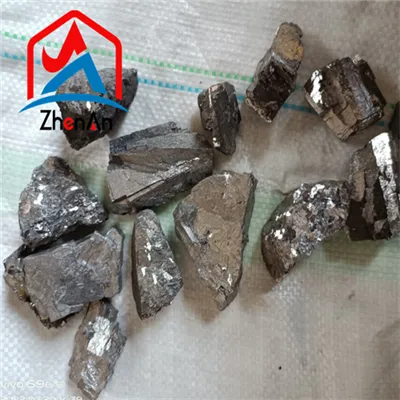


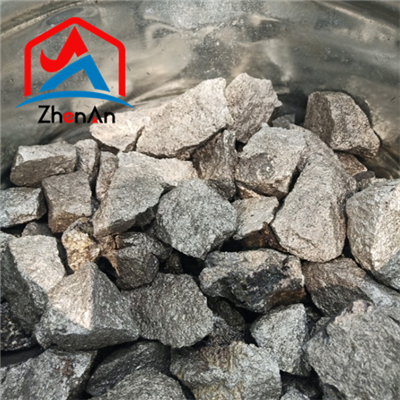


Steel Type — FeV Grade — V Addition Reference
| Steel type | Typical FeV grade | Indicative V addition | What FeV does |
|---|---|---|---|
| HSLA steel | FeV80 / FeV60 | 0.04–0.12% V | Precipitation strengthening, weldability |
| High-strength rebar | FeV80 / FeV50 | 0.02–0.08% V | Yield strength without excess carbon |
| Tool steel | FeV80 | 0.10–0.30% V | Wear resistance, red hardness |
| Spring steel | FeV80 / FeV60 | 0.08–0.20% V | Fatigue strength |
| Pipeline steel (X70/X80) | FeV80 / FeV60 | 0.04–0.10% V | Strength + toughness balance |
| Automotive steel | FeV80 / FeV60 | 0.03–0.10% V | Strength-to-weight |
| Alloy / bearing steel | FeV80 | 0.10–0.25% V | Hardness, hardenability |
| Steel casting | FeV50 / FeV40 | 0.05–0.15% V | Grain refinement, deoxidation |
Addition ranges are indicative; the optimum depends on your base composition, cooling rate and mechanical targets. Validate on trial heats.
precautions for product use
HSLA Steel
Ferrovanadium for HSLA steel delivers precipitation strengthening via V(C,N), letting low-alloy structural steels reach high yield with good toughness and weldability. High-strength low-alloy grades are one of the largest application segments for ferrovanadium. FeV80 or FeV60 is typical at 0.04–0.12% V. The grade selection depends on whether your melt shop prioritizes maximum vanadium recovery per kilogram of addition or lower unit cost for large tonnage campaigns. For mills producing structural plate, sections and line pipe, the strength-toughness balance achieved through vanadium microalloying often eliminates the need for more expensive molybdenum or nickel additions. The weldability improvement is particularly valuable in welded structural fabrications where cold cracking must be avoided.
High-Strength Rebar
Ferrovanadium for high-strength rebar supports microalloyed reinforcement bar that meets strength classes (e.g. BS 4449 / GB 1499.2 / ASTM A615) with lower carbon and better bendability. China's GB/T 1499.2-2018 rebar standard has been a notable driver for vanadium microalloying, promoting HRB400E, HRB500E and HRB600 grades that rely on controlled vanadium additions rather than increased carbon content to achieve higher strength. FeV80 or FeV50 is used at 0.02–0.08% V. Similar trends are visible in European and ASTM standards, where construction codes increasingly specify high-strength grades with improved ductility and weldability. The lower carbon equivalent of microalloyed rebar improves weldability on site, a critical factor for seismic-resistant construction.
Tool Steel
Ferrovanadium for tool steel improves wear resistance and red hardness through vanadium carbide formation. Tool steels operate under conditions of high mechanical stress and elevated temperature, where softening would rapidly degrade cutting or forming performance. The hard vanadium carbides that form during heat treatment remain stable at temperatures where other carbides would coarsen or dissolve. FeV80 at 0.10–0.30% V is standard for cold- and hot-work tool steels. The high vanadium content of FeV80 minimizes the total ferroalloy addition required to reach the target composition. In cold-work applications, the fine carbide distribution improves abrasive wear resistance; in hot-work grades, the stability of V-rich carbides at elevated temperature maintains cutting edge integrity.
Spring Steel
Ferrovanadium for spring steel raises fatigue strength and sag resistance. Springs are subjected to millions of load cycles, and failure typically initiates at surface or subsurface defects where stress concentrates. A finer grain structure, achieved through vanadium-controlled austenite grain size, distributes stress more evenly and delays crack initiation. FeV80 or FeV60 at 0.08–0.20% V is used in automotive and suspension springs. The precipitation-strengthening contribution from V(C,N) also helps maintain spring rate under sustained load, reducing the permanent set that can occur in lower-strength grades. Valve springs and suspension coils particularly benefit from the combination of high fatigue strength and adequate ductility.
Pipeline Steel (X70/X80)
Ferrovanadium for pipeline steel addresses the dual requirement of high strength and adequate toughness at low temperatures, particularly for sour-service grades where hydrogen-induced cracking resistance is a concern. Pipeline grades such as X70 and X80 must maintain ductile fracture behavior across a wide temperature window while resisting the effects of hydrogen sulfide in sour gas environments. FeV80 or FeV60 at 0.04–0.10% V is typical. The grain-refining effect of vanadium improves toughness in the heat-affected zone of welded joints, which is critical for line pipe girth welds. By enabling higher strength at lower carbon content, vanadium microalloying reduces carbon equivalent and improves field weldability — an essential requirement for long-distance pipeline construction.
Automotive Steel
Ferrovanadium for automotive steel helps reach strength-to-weight targets in advanced high-strength steels and structural components. As automotive producers face tightening emissions regulations and crash-safety standards, the pressure to reduce sheet thickness without sacrificing structural integrity continues to grow. FeV80 or FeV60 at 0.03–0.10% V supports formability with strength. Microalloyed automotive grades benefit from the weldability improvement that comes with lower carbon equivalent, which is essential for joining chassis components, body-in-white structures and crash-management systems. The ability to meet strength targets with leaner chemistry also reduces the alloying cost per vehicle.
Alloy / Bearing Steel
Ferrovanadium for alloy steel increases hardenability and hardness in engineering and bearing steels. In bearing applications, the combination of high hardness, adequate toughness, and dimensional stability under load depends on achieving a uniform microstructure with fine, well-distributed carbides. FeV80 at 0.10–0.25% V is common. The hardenability improvement from vanadium allows thicker sections to through-harden without excessive alloy content, reducing the need for costly quenching operations or additional alloy additions. In engineering steels, vanadium contributes to consistent mechanical properties across section sizes and improves machinability by promoting a uniform ferrite-pearlite microstructure.
Steel Casting
Ferrovanadium for steel casting refines the grain and deoxidises, improving soundness of cast components. Cast steels are prone to coarse as-cast grain structures that reduce toughness and machinability. Vanadium additions during the casting process restrict grain growth during solidification and subsequent cooling. FeV50 or FeV40 at 0.05–0.15% V is used where lower V unit is preferred. The deoxidising effect also contributes to cleaner castings with fewer inclusions. For large castings that cool slowly, the grain-refining benefit of vanadium is especially important because coarse grains form readily under slow cooling conditions and are difficult to refine by subsequent heat treatment alone.
Vanadium Microalloying and Grain Refinement
Vanadium microalloying works by precipitating nano-scale V(C,N) during recrystallisation and cooling. The precipitates pin dislocations and grain boundaries, raising strength without large carbon increases. Grain refinement — from vanadium's effect on austenite grain growth — further improves toughness and weldability. The right addition depends on composition, cooling rate and the target strength class; trial heats are recommended before specification change.
During solidification and subsequent thermomechanical processing, vanadium that remains in solution begins to precipitate as vanadium carbonitride, V(C,N), when the temperature falls into the range where the solubility product is exceeded. These precipitates are extremely fine — typically tens of nanometers in diameter — and form both during the austenite-to-ferrite transformation and within the ferrite matrix after transformation is complete. The carbonitride composition varies with the carbon and nitrogen content of the steel; higher nitrogen levels favor the nitride-rich end of the solid solution, while higher carbon levels shift the composition toward the carbide side.
The precipitation sequence matters. In conventionally processed steels, most V(C,N) forms during or after the gamma-to-alpha transformation. In thermomechanically processed steels — where controlled rolling is employed — strain-induced precipitation can occur in the austenite phase prior to transformation, further refining the final ferrite grain size by creating a dense distribution of pinning sites. This is why microalloyed steels processed on modern rolling mills often achieve higher strength-toughness combinations than equivalent chemistry steels processed by older routes.
Beyond precipitation strengthening, vanadium exerts a powerful grain-refining effect. By pinning austenite grain boundaries during reheating and rolling, vanadium limits the growth of austenite grains. When these fine-grained austenite grains transform to ferrite, the resulting ferrite grain size is also fine. Finer grains improve toughness according to the well-established Hall-Petch relationship, and they also improve weldability by reducing the hardenability of the heat-affected zone.
The grain-refining effect is particularly valuable in applications where weldability is a design constraint. High carbon content — the traditional route to high strength — increases carbon equivalent and raises the risk of cold cracking in welded joints. By substituting vanadium microalloying for carbon increase, mills can maintain or raise strength while actually reducing carbon equivalent. This is why HSLA pipeline grades, high-strength rebar for seismic construction, and automotive structural steels all increasingly rely on vanadium rather than higher carbon levels.
The effectiveness of a given vanadium addition depends on the base composition, the thermomechanical processing schedule, and the cooling rate after rolling or forging. High cooling rates — such as those achieved on modern accelerated cooling systems — favor finer precipitate distributions and stronger precipitation hardening. Conversely, slow cooling — as in heavy sections or air-cooled castings — produces coarser precipitates and less strengthening per unit of vanadium added.
Nitrogen content is another key variable. Vanadium has a strong affinity for nitrogen, and steels with higher nitrogen levels can achieve greater precipitation strengthening at the same vanadium addition. Some mills deliberately raise nitrogen content through process control or through the use of vanadium nitride (FeVN) rather than ferrovanadium, particularly in rebar applications where the cost-benefit favors the nitride route. The choice between FeV and FeVN depends on your nitrogen balance, available addition systems, and the specific strength targets for each product mix.
Trial heats remain the most reliable method for validating a new addition practice. Laboratory predictions and thermodynamic calculations provide a useful starting point, but the complex interplay of composition, temperature history, deformation schedule and cooling rate means that plant-specific validation is essential before committing to a specification change. The indicative addition ranges provided in the table above should be treated as starting points for trial programs, not as guaranteed outcomes.
Frequently Asked Questions
Q: How much ferrovanadium do I need for rebar?
Typical microalloyed rebar uses 0.02–0.08% V; the exact amount depends on your base chemistry and the strength class required.
Q: FeV80 or FeV50 for HSLA steel? Either works; FeV80 gives more V per kg (lower addition weight, less dilution). FeV50 is economical for large tonnage.
Q: Does particle size affect recovery?
Yes. Match size to your addition route — lumps for ladle, granules for continuous casting — to improve dissolution and recovery.
Q: Can ferrovanadium replace vanadium nitride?
They are different products; FeVN supplies N together with V for certain rebar routes. Choose based on your nitrogen balance.
ZhenAn International Co., Limited is one of the leading ferro vanadium manufacturers and suppliers in China. We warmly welcome you to wholesale discount ferro vanadium in stock here from our factory. All our products are with high quality and competitive price.
Ferro Vanadium For Smelting, Composition Of Ferrovanadium, Ferro Vanadium 50 For Chemical Catalysts