
Silicon Carbide Ball: Deoxidation and Warming in Iron and Steel
Leave a message
Introduction: The Silicon Carbide Ball as an Engineered Charge Material
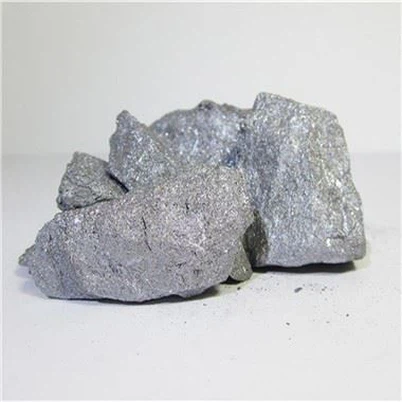
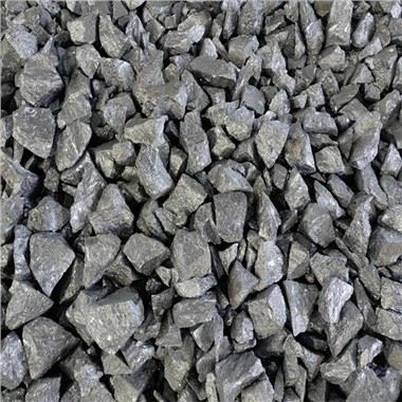
Silicon carbide is a compound of silicon and carbon with a theoretical composition of about 70.0% silicon and 30.0% carbon. In its abrasive and refractory forms it is supplied as crushed grain, powder and shaped bricks, but for iron and steel melts it is increasingly supplied as a bonded ball, sometimes called a briquette or a ball briquette. The ball is a manufactured shape: metallurgical-grade silicon carbide fines are mixed with a binding agent, pressed or rolled into a rounded form and cured, so that the particle size of the finished product is set by the die rather than by crushing.
That manufacturing step is the whole point of the product. A metallurgical melt cannot easily absorb loose fines, and dust blowing out of a scrap bucket or a charging chute is both a yield loss and a housekeeping problem. A ball of 20-50 mm can be weighed, counted, charged with the scrap and dropped through a chute without generating a dust cloud, and it dissolves at a predictable rate once it is under the slag. The ball therefore converts an awkward by-product stream into a standard charge component.
Three duties are normally expected of it. It deoxidises, it is a warming or heat-generating agent, and it is a secondary source of silicon and carbon for the melt. Which duty dominates depends on the furnace, the steel grade and where in the process the ball is charged.
Chemistry and Grades of Metallurgical Silicon Carbide
Silicon carbide for metallurgical use is graded mainly on silicon carbide content, with limits on free carbon, iron, alumina and moisture. The Chinese product standard GB/T 2480 covers silicon carbide, and metallurgical grades are commonly traded with a specified SiC content between about 60% and 90% with the remainder consisting of free carbon, unreacted silica, iron oxides and binder residue. Black silicon carbide is the grade normally used for metallurgical charging; the green grade is reserved for abrasive and refractory duties where purity matters more than cost.
| Nominal grade | SiC, % min | Free carbon, % | Iron as Fe2O3, % max | Moisture, % max | Typical duty |
|---|---|---|---|---|---|
| Metallurgical 90 | 90.0 | 3-5 | 1.5 | 0.5 | High-recovery deoxidation and silicon addition |
| Metallurgical 85 | 85.0 | 5-7 | 2.0 | 0.5 | Ladle and tapping deoxidation |
| Metallurgical 80 | 80.0 | 6-9 | 2.5 | 0.8 | General steel deoxidation |
| Metallurgical 70 | 70.0 | 8-12 | 3.0 | 0.8 | Recarburising plus silicon addition in iron |
| Metallurgical 60 | 60.0 | 10-15 | 3.5 | 1.0 | Cupola and foundry silicon carry-over |
The crystalline form matters to dissolution behaviour but not to the grade name. Industrial silicon carbide crystallises either in the hexagonal alpha form, which is what the Acheson furnace produces and what most metallurgical product consists of, or in the cubic beta form, which is finer and more reactive. Most metallurgical ball is made from alpha material with a controlled grain size, and the binder is chosen so that the ball keeps its shape in storage yet breaks down quickly once it is in the bath.
Two specification points catch buyers out. First, the moisture limit is not a formality: bonded balls absorb water, and wet balls burst when they hit molten metal, which is a genuine safety hazard as well as a yield loss. Second, free carbon should be declared separately from total carbon, because free carbon recarburises the melt while the carbon bound as silicon carbide does not dissolve in the same way.
Physical Properties and How the Ball Form Is Built
Silicon carbide is extremely hard and refractory: its Mohs hardness is about 9 to 9.5, its density is approximately 3.2 g/cm3, and it dissociates rather than melting cleanly at temperatures in the region of 2700 degrees Celsius and above. Those properties explain why the material must be shaped with a binder: a loose powder of such a hard, high-melting solid is difficult to feed into a melt uniformly.
The ball therefore combines three separate engineering decisions. The grain size of the silicon carbide powder in the mix controls how quickly the ball breaks down. The binder type and content control green strength, drop strength and moisture uptake. The die geometry controls the nominal diameter and the mass of each piece, which in turn lets the melt shop calculate an addition by weight rather than by volume.
Typical diameter: 20-50 mm for steel and iron melting, with 10-30 mm grades for smaller furnaces and for cored or gravity feeding systems.
Drop strength: the practical acceptance test is a drop onto a steel plate from a defined height without shattering, which predicts how the ball behaves in a charging bucket.
Bulk density: lower than solid silicon carbide because of binder and internal porosity, which is why a ball supplier should declare bulk density alongside chemical analysis.
Moisture uptake: measured as the mass gain after defined humidity exposure, the single most useful storage-life indicator for a bonded ball.
Because porosity lowers bulk density, the ball also floats more readily on a slag layer than dense lump material does. That is an advantage in a covered arc furnace where the ball sits on the slag and reacts with the slag phase, and a disadvantage in an open ladle where the aim is to get silicon and carbon into the metal before the slag absorbs them. This is why ball product is usually charged with scrap rather than thrown onto a quiet ladle bath.
Deoxidation Behaviour in Steel and Iron Melts
When a silicon carbide ball enters a molten bath, the silicon carbide dissociates and its silicon and carbon enter solution. The dissolved silicon then reacts with dissolved oxygen to form silica, and the dissolved carbon reacts with dissolved oxygen to form carbon monoxide. Both reactions take oxygen out of the steel, and both are strongly exothermic, which is the origin of the warming effect that gives the ball a second use.
Compared with the more common deoxidisers, silicon carbide has one clear advantage and one clear limitation. The advantage is that it supplies two active elements in a single addition and releases heat while doing so, which is valuable in a cold-charge electric furnace or a cupola where thermal budget is tight. The limitation is that the carbon it releases raises the carbon content of the bath, which rules it out for low-carbon and ultra-low-carbon steel grades unless the addition is small and the carbon is deliberately accounted for.
| Material | Active elements delivered | Thermal effect | Carbon risk | Best suited to |
|---|---|---|---|---|
| Silicon carbide ball | Silicon and carbon | Strongly exothermic | Significant, must be booked | Electric furnace and cupola charging, high-carbon and medium-carbon grades |
| Ferrosilicon lump | Silicon | Mildly exothermic | Negligible | General deoxidation and silicon alloying |
| Aluminium | Aluminium | Strongly exothermic | None | Killing of low-carbon steel |
| Graphite or petroleum coke | Carbon | Endothermic dissolution | Deliberate | Recarburisation only |
The practical rule is that silicon carbide is a charging-stage material, not a final finishing material. It is at its most efficient when it is added early, mixed with scrap or charged into a heat that is still short of silicon, so that the silicon has time to dissolve and the carbon has time to be absorbed or reduced as intended. Used late in the ladle, a large share of the benefit is lost to the slag.
Use as a Warming and Heat-Generating Agent
The exothermic oxidation of silicon and carbon makes a silicon carbide ball an effective warming agent in processes that run on a tight thermal margin. In an electric arc furnace, oxygen lancing and long power-off periods cool the bath; a charge of silicon carbide briquettes releases heat exactly where it is needed and simultaneously adds silicon. In a cupola, adding silicon carbide to the charge raises tapping temperature and improves silicon recovery, because the material releases heat as it oxidises while still delivering silicon to the iron.
A warming addition is judged by the temperature rise it produces in a defined bath mass rather than by any single catalogue number, because the usable heat depends on how much of the silicon and carbon is actually oxidised in the bath rather than lost to the slag or the off-gas. The useful control variables are the mass of ball charged per tonne of metal, the point of addition, and the oxygen potential of the bath at that moment. Recording the temperature before and after a trial addition of known mass on each furnace is the only reliable way to build a plant-specific figure.
Warming additions should also be checked against the carbon specification. A heat that is close to its carbon upper limit cannot accept a large silicon carbide charge, however attractive the thermal benefit looks, and the melt shop should therefore keep a separate silicon-bearing warming option such as ferrosilicon available for those heats.
Silicon Carbide in Cupola and Foundry Iron Melting
In foundry work the ball has an additional role beyond deoxidation and heat. Molten cast iron dissolves oxygen readily, and a high oxygen content interferes with graphite nucleation, which is why foundries add silicon-bearing charge materials rather than relying on the base iron alone. Silicon carbide offers a low-oxygen-potential source of silicon that dissolves progressively as the charge melts, and foundries use it together with conventional inoculation practice to improve graphite morphology and reduce chill.
Typical practice is to place silicon carbide briquettes in the charge mix rather than on the ladle, so that the material is exposed to the full melting cycle. In an induction furnace, where the aim is usually chemistry correction rather than bulk heat generation, the addition is smaller and is made before the final silicon trim, because the carbon released by the ball has to be balanced against the target carbon of the iron.
Cupola practice: briquettes are charged with coke and metal to raise silicon recovery and tapping temperature.
Induction furnace practice: used as a silicon carrier that is less prone to dust loss than powdered alternatives.
Foundry quality effect: lower oxygen in the melt supports graphite nucleation and reduces chill depth.
The grade choice follows the duty. A foundry balancing silicon and carbon targets on a medium-grade iron will normally use a 70-80% silicon carbide ball, while a melt shop using the ball purely as a heat and silicon source for high-carbon steel may prefer an 85-90% grade to minimise the free-carbon load per unit of silicon delivered.
Charging, Dissolution and Process Control
Because the ball is a bonded shape, its dissolution is slower and more even than that of loose fines, but it is not instantaneous. Charging the ball with the scrap exposes it to the full heating cycle and gives the longest contact time; charging it onto a slag layer during refining exposes it to a slag that may itself consume the silicon; injecting or dropping it into a quiet ladle places it near the surface where it can be lost to the slag without ever reaching the metal.
Process control therefore concentrates on three measurements. The silicon and carbon delivered per tonne of metal are calculated from the certified analysis and the mass charged. The temperature effect is measured by before-and-after temperature readings on trial heats. The recovery is confirmed by comparing the analysed silicon and carbon in the finished heat with the calculated additions from all sources, so that the contribution of the ball is separated from that of ferrosilicon, scrap and recarburiser.
Weighing discipline: charge by mass, not by count, because ball mass varies with moisture and binder content.
Moisture check: reject wet or visibly cracked balls and dry store before charging.
Balance sheet: account for the ball's carbon in the same way as an intentional recarburiser addition.
Repeatability: fix the point of addition for a given furnace so that recovery figures remain comparable between heats.
Plants that follow this discipline generally find that the ball replaces part of both the ferrosilicon and the recarburiser charge, which is where the commercial case for the product is actually made. The saving comes from fewer separate additions and less dust loss, not from the silicon carbide itself being cheaper per unit of silicon on a like-for-like basis.
Size, Packaging, Storage and Safety
Size ranges for charge materials in iron and steel melting are normally agreed against the ferroalloy size-grading conventions of GB/T 13247, which fixes nominal ranges and the permitted proportions of undersize and oversize material. A ball product specification should therefore state the nominal diameter, the tolerance on that diameter, the permitted proportion of broken pieces, and the moisture content. Fine silicon carbide grain for abrasive and refractory applications is graded according to ISO 9286, which is a useful reference when a buyer needs to compare the underlying powder with a strict size distribution.
| Property | Typical requirement for charging balls | Test or basis |
|---|---|---|
| Nominal diameter | 20-50 mm (10-30 mm for small furnaces) | Sieving, size rules of GB/T 13247 |
| SiC content | 60-90% depending on grade | Chemical analysis against GB/T 2480 grade |
| Moisture | 0.5-1.0% max | Mass loss on drying a representative sample |
| Broken pieces | Agreed percentage limit after transport | Visual inspection and sieving at receipt |
| Marking | Grade, batch and net mass per unit | Packaging conventions of GB/T 3650 |
Storage and safety requirements follow from the material rather than from the shape. Silicon carbide is chemically stable and does not react violently with water at ambient temperature, but the binder in a bonded ball can take up moisture, so bags should be stored under cover on dry flooring and opened units should be used promptly. Dust from broken balls is a respiratory irritant and is hard and abrasive, so extraction at the charging point and appropriate personal protective equipment are standard practice. Wet or damp balls must never be charged into molten metal, and contact between molten metal and standing water in the charging area should be eliminated as a matter of routine.
Quality Control and Acceptance for a Ball Product
Acceptance of a manufactured ball has a chemical side and a physical side, and the physical side carries more weight than it does for lump ferroalloys because the product is an engineered shape. Sampling of the silicon carbide content should follow the general principles of GB/T 4010 for ferroalloys and ISO 3713 for international trade, taking increments from several units across the lot and reducing them to a representative analytical portion. Because binder is not uniformly distributed, increments should be taken from complete balls rather than from the loose fines at the bottom of a bag.
The physical checks are quick and worth performing on every receipt. Measure the diameter of a random sample of balls against the agreed nominal size. Weigh a sample to confirm piece mass consistency. Drop a sample onto a steel plate from the agreed height and count the pieces that shatter, which predicts behaviour in the charging bucket. Dry a weighed sample to determine moisture, and note any balls that are cracked, crumbly or discoloured. Retain a sealed sample of the lot together with the mill certificate for the agreed warranty period.
On the process side, the decisive verification is the heat balance. If the analysed silicon and carbon of the finished heat are consistently below the calculated total from all charge sources, the shortfall indicates that the ball is being lost to the slag, that it is wet, or that its declared silicon carbide content is overstated. That single calculation converts a supplier claim into a plant-verifiable number, and it should be run on the first three heats of every new lot before the material is released to routine use.
FAQ
Q: What is a silicon carbide ball used for?
It is charged to iron and steel melts as a combined deoxidiser, silicon and carbon carrier, and warming agent. It is normally charged with scrap or in the furnace charge rather than added to a quiet ladle, because the carbon it releases must be balanced against the target carbon of the heat.
Q: What silicon carbide content is normal in a metallurgical ball?
Metallurgical grades are commonly traded between 60% and 90% silicon carbide, with free carbon, iron as Fe2O3 and moisture declared separately. Content is specified against the grade in GB/T 2480, and the balance consists of free carbon, unreacted silica and binder residue.
Q: Why is the ball form preferred over silicon carbide powder or fines?
A bonded ball can be weighed, charged with scrap and dropped through a chute without generating a dust cloud, and it dissolves at a more predictable rate than loose fines. The shape also reduces the material that is blown out of the bucket or lost to housekeeping.
Q: Does silicon carbide ball add carbon to the steel?
Yes. Silicon carbide dissociates in the melt and releases both silicon and carbon, and the carbon oxidises to carbon monoxide while removing oxygen. The free carbon content must therefore be declared and accounted for in the carbon balance, which is why the product is not used for ultra-low-carbon grades.
Q: How is the warming effect of a silicon carbide ball measured?
By the temperature rise produced in a defined bath mass on that specific furnace, recorded before and after a trial addition of known mass. The usable heat depends on how much silicon and carbon actually oxidise in the bath rather than being lost to the slag or off-gas.
Q: What should be checked when receiving a shipment of silicon carbide balls?
Confirm the diameter against the agreed nominal range, check piece mass consistency, run a drop test to assess shatter resistance, measure moisture by drying a sample, and take full balls as increments for silicon carbide analysis in line with the ferroalloy sampling principles of GB/T 4010 or ISO 3713.
Summary of Practical Selection Rules
The silicon carbide ball is best understood as a charge engineering product rather than as a simple ferroalloy substitute. Its value comes from three things a powder cannot deliver: a controlled, dust-free feed; a combined supply of silicon and carbon that also generates heat; and a dissolution rate that can be set by grain size and binder during manufacture.
Selection should follow the duty. Use a high-grade 85-90% ball where the priority is silicon recovery and deoxidation with minimum free carbon. Use a 70-80% grade where the carbon is welcome, as in foundry iron or high-carbon steel. Size the ball to the charging system, 20-50 mm for scrap buckets and chutes and 10-30 mm for smaller furnace and feeding equipment. Store dry, charge by mass, account for the carbon in the heat balance, and verify the delivered silicon and carbon against analysis on the first heats of every lot.